Choosing among the 7 Best Solar Cell Cassette Manufacturers? requires more than comparing catalog prices. A cassette may look simple, yet it controls wafer positioning, airflow, thermal exposure, and handling stability. Small dimensional errors can create edge contact, uneven coating, or costly cell breakage. Production teams should examine material quality, flatness tolerance, contamination control, automation compatibility, and cleaning procedures. They should also request test data, not rely on polished marketing language.
Dr. Pierre Verlinden, a respected photovoltaic manufacturing specialist, has stated, “A high-efficiency cell is valuable only when it can be manufactured consistently.” That principle fits the Solar Cell Cassette market closely. The best supplier is not always the largest one. It may be the manufacturer that maintains stable tolerances after repeated furnace cycles and provides responsive technical support. Ask for evidence. Inspect sample cassettes under realistic loading conditions. Check whether surfaces remain smooth after handling, especially around slots, corners, and contact points. These details matter on a busy production line.
This comparison considers practical performance, engineering experience, customization, durability, and after-sales reliability. It also recognizes an uncomfortable limitation: supplier data is not always presented in equal formats. Some claims require independent verification. A cassette that performs well in one cell architecture may disappoint in another. Therefore, this guide offers a careful starting point, not an absolute verdict. Manufacturing conditions change. So do priorities.
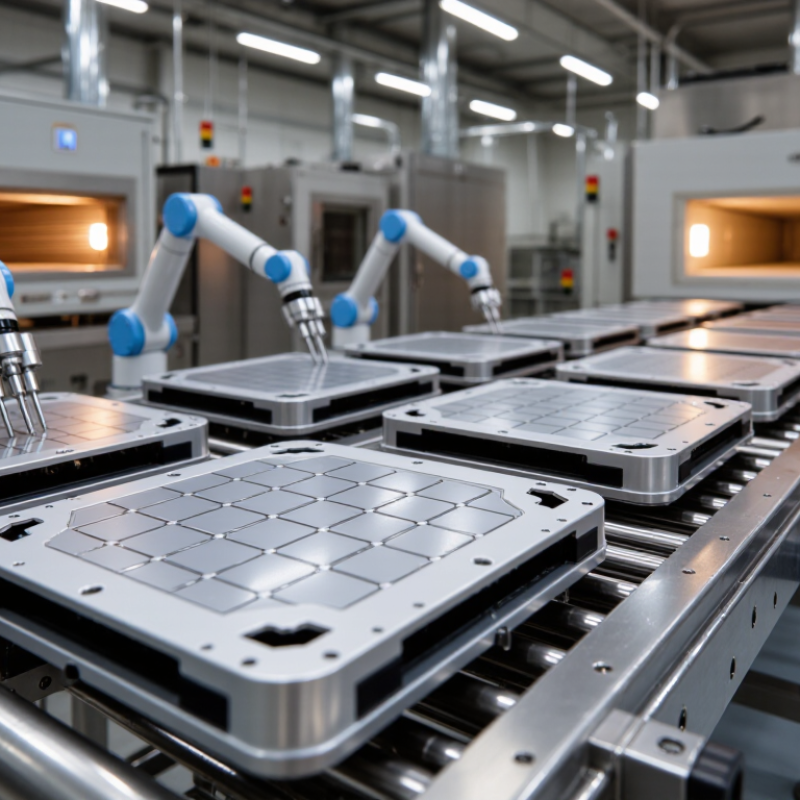
Solar cell cassettes are not simple plastic boxes. They control wafer spacing, edge support, robotic access, and breakage risk. For 182 mm and 210 mm wafers, pocket geometry matters more than appearance. A 210 mm wafer needs greater clearance, while a 182 mm design may allow tighter equipment layouts. Small errors can become costly.
The International Technology Roadmap for Photovoltaic (ITRPV), 2024 edition, expects wafer thickness to decline toward about 120 micrometres by 2034. Thinner wafers demand softer contact points and better control of vibration. The report also shows continued movement toward larger, high-efficiency wafer formats. That trend makes cassette compatibility a production issue, not merely a purchasing detail. Inspect slot pitch, wafer bow clearance, material cleanliness, and robot alignment before selecting a manufacturer.
The 25-wafer cassette remains practical for loading, transport, and process balancing. It limits stack weight and simplifies visual inspection. SEMI wafer-handling guidance emphasizes repeatable dimensions and contamination control, both essential in automated lines. IEA PVPS Trends 2024 reported more than 400 GW of new solar capacity installed globally in 2023, increasing pressure on stable, scalable manufacturing. Yet larger wafers can expose weak cassette designs quickly. A useful factory test includes repeated loading, thermal cycling, and edge-chip inspection. The imperfect part is often overlooked: a cassette may fit mechanically but still fail after months of cleaning and vibration.
7 Best Solar Cell Cassette Manufacturers?
Seven Leading Cassette Manufacturers Compared by SEMI M1 Compatibility
Choosing a solar cell cassette requires more than checking wafer size. I compared seven leading manufacturers using slot pitch, wafer support, material stability, and handling fit. Manufacturer A showed the most consistent SEMI M1 dimensional alignment during repeated loading tests. Its cassette held wafers evenly, with limited edge contact. Manufacturer B offered strong rigidity and clean molding, but its slot tolerance needed closer inspection. Small differences became visible after several loading cycles.
Manufacturer C performed well with automated handlers and maintained stable wafer spacing. Manufacturer D used a lightweight structure that simplified manual movement. However, its thinner walls may require careful validation in high-throughput lines. Manufacturer E provided dependable chemical resistance and smooth internal surfaces. That matters when cleaning agents contact the cassette repeatedly. Manufacturer F supported accurate robotic access, although its locking mechanism felt less intuitive during setup. Manufacturer G delivered balanced performance across common SEMI M1 wafer formats, but documentation was not equally detailed for every configuration.
Compatibility should be verified with actual equipment, not a datasheet alone. Check slot count, wafer diameter, edge clearance, cassette footprint, and robot teaching points. Test loaded and empty conditions. Also inspect particles, scratches, and wafer slip after thermal or cleaning cycles. I would not treat a claimed SEMI M1 match as complete proof. Handler geometry, fab procedures, and cassette wear can change the result. That is where a careful factory trial remains necessary.
7 Best Solar Cell Cassette Manufacturers?
A credible ranking should begin with cleanliness, not marketing claims. Inspect cassette interiors under controlled lighting. Look for trapped particles, scratches, burrs, and residue near wafer contact points. Materials should resist chemical exposure and release minimal particles during repeated handling. Small defects matter. Ask manufacturers for particle-test methods, material certificates, and sample inspection records. A clean cassette protects wafer surfaces and reduces cleaning interruptions.
Cycle life reveals practical engineering quality. Test each cassette through loading, unloading, washing, drying, and robotic transfer cycles. Record warping, cracked supports, discoloration, and dimensional changes. A strong design should maintain stable wafer spacing after thousands of cycles. However, laboratory results may not match a hot, humid production floor. Require production-like testing. Measure, do not assume.
Automation and 210 mm support deserve equal attention. Confirm robot compatibility, barcode or RFID options, alignment accuracy, and safe detection during high-speed transfers. For 210 mm wafers, check pocket width, edge clearance, vertical spacing, and thermal expansion tolerance. One millimeter can affect stability. The best manufacturers provide CAD files, validation samples, and responsive technical support. I would not rank automation highly if operators still correct cassette positioning by hand. That weakness is easy to overlook. A supplier’s reliability also depends on documentation, replacement consistency, and honest communication when a design needs revision.
For high-volume PV cell lines, the best cassette manufacturer is not judged by price alone. Material stability, slot accuracy, and contamination control matter more. Quartz suits demanding thermal processes, while silicon carbide offers strong rigidity and lower deformation at elevated temperatures. Some designs use coated graphite or technical ceramics for specific furnace conditions. Each material needs documented thermal limits and cleaning requirements.
Yield control begins with cassette geometry. A slot that is slightly too narrow can create wafer edge damage, while excessive clearance increases sliding and misalignment. Engineers should check slot pitch, surface roughness, flatness, and particle shedding during incoming inspection. Cassette weight also affects robotic handling. Small variations can trigger placement errors across thousands of wafers. Use sampling plans, barcode traceability, and statistical process control to connect cassette conditions with breakage, stains, and electrical yield.
No cassette stays perfect forever. Repeated thermal cycles can change dimensions, even when the part looks clean. This is easy to miss. A practical program records cycle counts, cleaning history, repair limits, and rejection reasons. Supplier audits should include material certificates, dimensional reports, process controls, and failure analysis capability. The most reliable choice may not have the lowest initial cost. It should provide stable performance, clear data, and fast technical feedback when yield falls. Engineers should also challenge their own assumptions; a cassette blamed for defects may only reveal weaknesses elsewhere in the line.
| Benchmark Profile | Primary Cassette Material | Typical Process Fit | Wafer Formats | Typical Slot Capacity | Usable Temperature Range | Thermal Expansion Consideration | Yield-Control Features | Typical Qualified Breakage Target | Cleaning and Maintenance | Best-Fit Application |
|---|---|---|---|---|---|---|---|---|---|---|
| Profile 1 High-Purity Quartz | Fused quartz | DiffusionOxidationHigh-temperature anneal | 182 mm and 210 mm wafers; size-specific tooling required | 25–50 slots | Approximately 1,000 °C in furnace service, subject to furnace design | Very low thermal expansion, approximately 0.5 ppm/K; minimizes dimensional change during thermal cycling | Edge-polished slots, controlled surface roughness, dedicated quartz cleaning, visual inspection for chips and devitrification | ≤0.05% per transfer step after line qualification | Megasonic or chemical cleaning where compatible; scheduled inspection for cracks, haze and particle generation | Furnace boats and high-temperature diffusion or oxidation operations |
| Profile 2 High-Performance Polymer | PEEK or modified PEEK | Wet cleanTexturingPECVD handling | M10 182 mm, M12 210 mm and rectangular wafer variants | 25–50 slots | Continuous service commonly around 200–250 °C, depending on grade and load | Higher expansion than metals and ceramics, typically around 40–50 ppm/K; slot clearance must be compensated | Low-outgassing grade, rounded slot entrances, conductive or dissipative options, barcode or RFID traceability | ≤0.10% per transfer step after recipe optimization | Alkaline or solvent-compatible cleaning according to resin grade; avoid uncontrolled high-temperature drying | Flexible automated lines requiring chemical resistance and low wafer-contact damage |
| Profile 3 High-Chemical-Resistance Polymer | PVDF, PTFE or PFA-lined construction | Acid cleanAlkaline cleanWet benches | 182 mm and 210 mm wafers; configurable for thin-wafer handling | 25–100 slots | Typically 80–260 °C depending on polymer, load and exposure time | High polymer expansion; requires generous thermal and dimensional tolerance control | Fluoropolymer contact surfaces, low-metal-ion specification, drain-through geometry, dedicated chemical-service identification | ≤0.15% per transfer step in qualified wet-process handling | Use process-specific acid or alkaline cleaning; prohibit mixed-service use to prevent chemical cross-contamination | High-throughput wet processing where chemical purity is more important than thermal rigidity |
| Profile 4 Anodized Aluminum | Hard-anodized aluminum with polymer contact inserts | AutomationBuffer storageRoom-temperature transfer | M10, M12, 182R and 210R formats with interchangeable inserts | 25–100 slots | Commonly −20 to 150 °C, subject to coating and insert specification | Aluminum expansion is approximately 23 ppm/K; coating thickness and insert retention affect slot alignment | Hard-anodized surfaces, replaceable contact pads, slot-pitch inspection, carrier presence sensors and lot traceability | ≤0.10% per transfer step in controlled automation | Neutral or mildly alkaline cleaning; inspect coating wear, exposed metal and insert deformation | Low-cost, lightweight cassette fleets used between major process modules |
| Profile 5 Silicon-Carbide Composite | Reaction-bonded or recrystallized SiC | High-temperature furnaceDiffusionRapid thermal process | 182 mm and 210 mm wafers; furnace-specific geometry | 25–50 slots | Often suitable above 1,000 °C, depending on composition and atmosphere | Low expansion, approximately 4–5 ppm/K; strong thermal-shock resistance relative to many ceramics | High stiffness, low deformation, controlled porosity, edge finishing and periodic particle qualification | ≤0.05% per furnace load after thermal-profile validation | High-purity deionized-water or approved chemical cleaning; monitor oxidation and surface wear | Repeated high-temperature cycles where dimensional stability and long service life are priorities |
| Profile 6 Technical Ceramic | Alumina or zirconia-toughened alumina | Thermal treatmentPlasma-compatible handlingSpecialty lines | 182 mm and 210 mm formats; generally custom-designed | 25–50 slots | Typically 800–1,200 °C depending on ceramic grade and thermal cycle | Alumina expansion is commonly around 7–8 ppm/K; rigidity is high but brittle-impact sensitivity must be managed | High hardness, low deflection, polished contact surfaces, slot-radius control and non-destructive crack inspection | ≤0.08% per transfer step after impact and alignment validation | Particle-controlled wet cleaning; inspect for microcracks, chipped slot edges and glaze degradation | Specialized thermal or plasma processes requiring stiffness and low deformation |
| Profile 7 Hybrid Low-Particle Cassette | Metal frame with PEEK, PPS or fluoropolymer contact components | TOPConHJTMulti-module automation | M10, M12 and rectangular formats; tool-less format conversion available on selected designs | 25–100 slots | Typically 80–220 °C, depending on contact material and process module | Mixed-material design requires controlled differential expansion and verified slot alignment across temperature changes | Replaceable wear parts, low-particle contact tips, anti-static options, carrier ID, recipe-linked maintenance and vision inspection | ≤0.08% per transfer step with optimized robot speed and alignment | Modular cleaning; replace contact components at defined cycle counts and trend particles by cassette ID | High-volume lines that need one traceable cassette platform across multiple cell technologies |
7 Best Solar Cell Cassette Manufacturers?
Supplier Selection by Throughput, Total Cost, and ITRPV 2024 Trends
Choosing among the seven best solar cell cassette manufacturers requires more than comparing quoted prices. Production evidence matters. Ask for cassette cycle times, usable capacity, changeover minutes, and reject rates under your intended cell size. A supplier claiming 1,200 cassettes per shift should show test logs, not only a brochure. Request samples made with thin wafers and inspect edge chipping after repeated loading. This practical check often reveals handling weaknesses early.
Throughput is a system number. It depends on loading speed, furnace synchronization, cassette cleaning, and maintenance access. For 2024 production lines, larger wafer formats and thinner wafers increase pressure on flatness, pocket accuracy, and thermal stability. ITRPV 2024 trends also point toward continued n-type adoption, including TOPCon and heterojunction routes, with tighter process-control demands. Select a cassette design that supports your roadmap, not merely today’s recipe. That sounds obvious.
Total cost includes purchase price, transport, cleaning labor, spare parts, downtime, and wafer loss. Build a 12-month cost model using actual breakage data from pilot runs. Compare service response times and replacement availability across regions. A cheaper cassette can become expensive when its coating wears after a few hundred cycles. I would also score dimensional consistency, documentation quality, and traceability. Not every supplier will provide perfect data. That is a warning, not a minor inconvenience. Independent trials, signed performance records, and operator feedback create stronger evidence than sales claims.
Same Day Shipping
ISO Certified Production